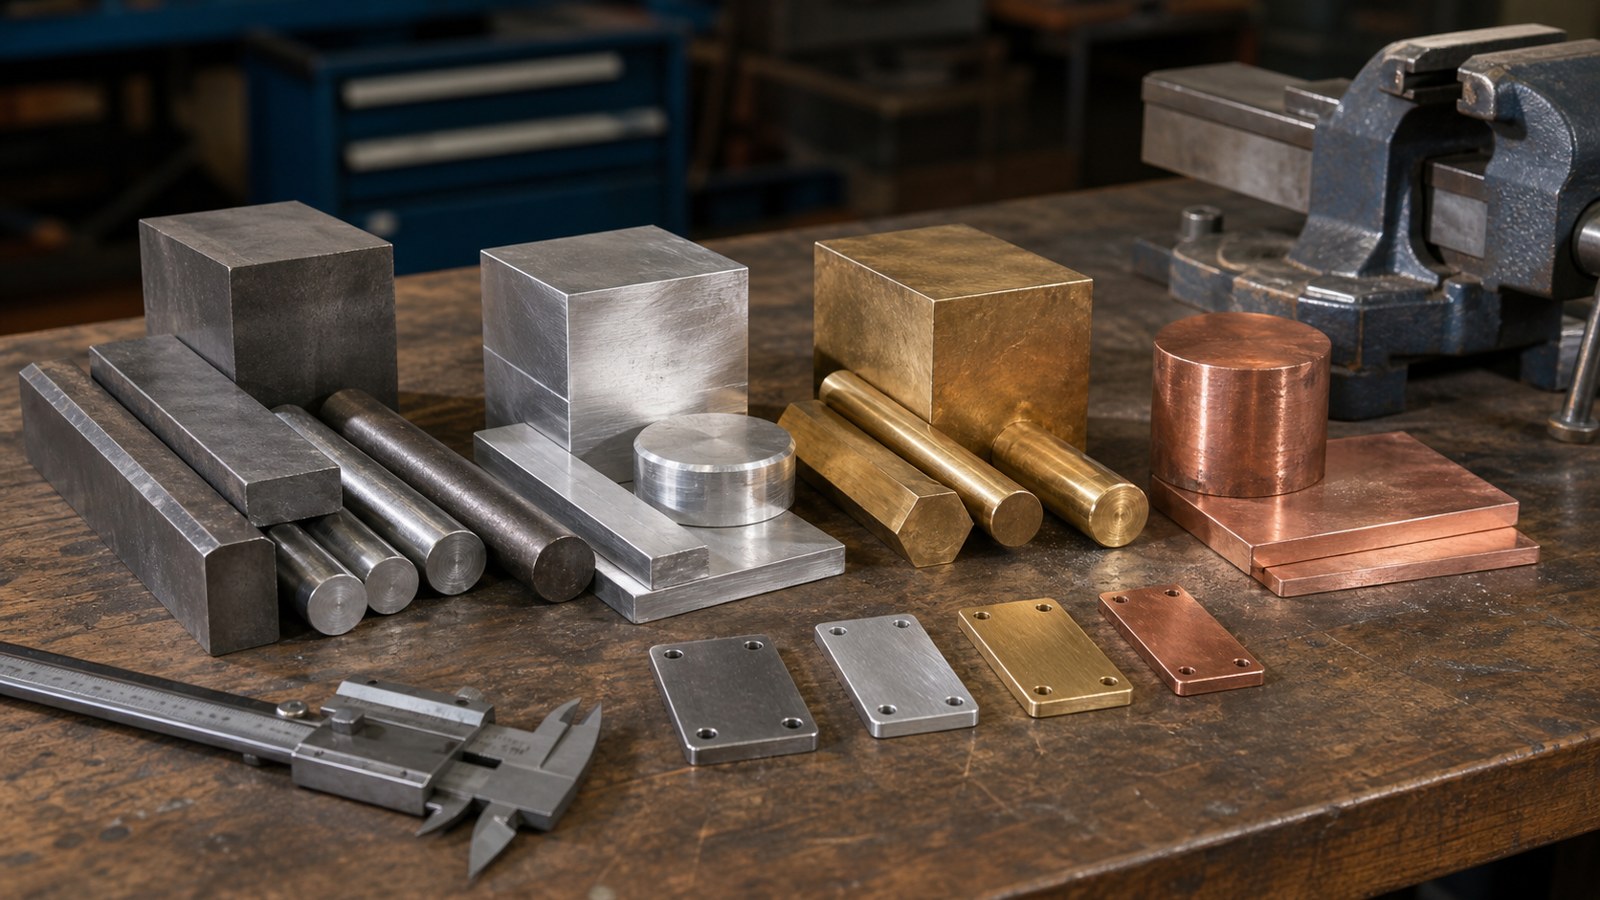
Ferrous and Non-Ferrous Metals Behave Differently in Fabrication
Metals are often divided into ferrous and non-ferrous groups. Ferrous metals contain iron and include carbon steel, stainless steel, cast iron, and many tool steels. Non-ferrous metals do not rely on iron as the main element and include aluminum, copper, brass, bronze, titanium, zinc, magnesium, and nickel alloys. The distinction matters because it affects strength, corrosion behavior, weight, magnetism, weldability, machinability, cost, finishing, and how the material performs in service.
A: Clear design intent, suitable material, controlled setup, safe workflow, and repeatable inspection.
A: It shows how the material and tool settings behave before the final part is at risk.
A: No. Tighter tolerance costs more and only helps when the function requires it.
A: Tool wear, speed, feed, abrasive choice, heat, vibration, or weak support can all contribute.
A: Heat, internal stress, uneven removal, poor clamping, or forming pressure can move material.
A: Use templates, mark clearly, cut oversize when appropriate, and inspect before each irreversible step.
A: Prototypes test ideas, while production work controls repeatability.
A: Surface prep, cleaning, masking, curing, and inspection often require more time than the main cut.
A: Ventilation and dust control are often overlooked until a process creates fumes or fine particles.
A: Confirm fit, function, finish, documentation, and any maintenance needs.
What Ferrous Means
Ferrous metals contain iron. Many are magnetic, though not all stainless steels behave the same way. Ferrous metals are common because they can be strong, affordable, and widely available.
Carbon steel is used for frames, brackets, tools, structures, machinery, and countless fabricated products. Its weakness is that it can rust without coating, plating, oil, or another protective strategy.
In shop terms, ferrous affects how the fabrication work moves from a drawing into a part that can be held, cut, checked, and finished. For this fabrication project, that keeps the choice grounded in the actual build rather than a generic preference. It also gives the builder a specific thing to watch while ferrous moves from plan to shop work.
The detail deserves a small reality check before the next operation. A sample, dry fit, or first-piece inspection can show whether the plan is behaving as expected. A quick measurement or shop note at this point can prevent a much larger correction later and keep the next operation from hiding the problem. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
That check gives the team a concrete signal instead of a vague impression. If fit, edge quality, release, alignment, or finish starts to drift, the process can be corrected early. It also makes responsibility clearer when design, setup, cutting, and finishing overlap. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
The practical next step is to document the setting, mark the feature clearly, and keep the result tied to the drawing so the same choice can be repeated later. The result is a ferrous decision that can be inspected, explained, and improved on the next run without rebuilding the whole plan. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
Carbon Steel
Carbon steel ranges from low-carbon mild steel to harder high-carbon grades. Mild steel is easy to weld, form, machine, and fabricate, which makes it a shop staple.
Higher-carbon steels can be stronger or harder but may be less forgiving during welding and forming. Heat treatment and alloy content change performance significantly.
For this fabrication project, carbon steel is not an isolated detail. It influences material selection, setup time, tool access, and the amount of correction needed after the main operation. That keeps the work tied to fit, finish, safety, and cost instead of treating the detail as decoration. It also gives the builder a specific thing to watch while carbon steel moves from plan to shop work.
A builder can treat this part of the work as a decision point: continue with the current setup, adjust the geometry, change the tool, or run a smaller trial first. When carbon steel is checked early, the builder has more options and less pressure to force a fix at the end after the part is already committed. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
That decision is easier when the part is checked against the real stock and the real mating surfaces rather than only against an ideal model. It also gives the next person in the workflow a clearer reason for the chosen setup. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
Good notes matter here because they turn one successful setup into a repeatable method for the next part, batch, repair, or revision. For this fabrication project, that record can be reused when the material, tooling, or quantity changes and the shop needs the same result again. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
Stainless Steel
Stainless steel contains chromium, which helps form a protective oxide layer. It is valued for corrosion resistance, clean appearance, and durability.
Different stainless grades have different strength, corrosion resistance, magnetism, machinability, and weldability. The right grade depends on environment, cleaning, temperature, and fabrication method.
The value of stainless steel becomes clear when the project reaches the bench. Small differences in thickness, radius, heat, clamp pressure, or surface prep can change the result. For this fabrication project, the payoff is fewer surprises when the part reaches assembly or finishing. It also gives the builder a specific thing to watch while stainless steel moves from plan to shop work.
Instead of waiting for final assembly to reveal the issue, the shop can look for early signs: uneven fit, rough edges, distortion, poor release, or extra finishing work. A short pause here can protect the schedule because the correction is still small and visible. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
Those signs help separate a design issue from a setup issue. The fix may be a cleaner drawing note, a different sequence, a new fixture, or a more suitable material. That makes stainless steel a practical control point instead of a vague shop preference, especially when multiple people touch the same job. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
Handled this way, the topic becomes a working checklist rather than filler. It points to the specific shop condition that needs attention before the job advances. The next build starts from a known condition rather than from memory or guesswork. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
Cast Iron and Tool Steel
Cast iron contains more carbon and is often used for machine bases, cookware, engine parts, and components that benefit from damping and compressive strength.
Tool steels are engineered for hardness, wear resistance, toughness, or heat resistance. They are used for dies, molds, cutters, punches, and tooling rather than general structures.
Cast iron and tool steel also shapes communication. Designers, programmers, fabricators, and finishers need to know which surfaces matter and which dimensions have room to breathe. That context helps the team avoid spending time on details that do not change performance. It also gives the builder a specific thing to watch while cast iron and tool steel moves from plan to shop work.
When that priority is clear, the shop can spend effort where it improves the finished part instead of chasing precision or polish in the wrong place. Checked early, cast iron and tool steel can guide a better fixture, clearer drawing note, or cleaner finishing plan before the expensive steps begin. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
The best review point is simple: compare the part to its function, not just to its appearance. Fit, strength, safety, and service conditions decide whether the work is ready. The process also becomes easier to teach because the reason behind the step is visible. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
If the review exposes a problem, changing one variable at a time keeps the lesson useful. That habit prevents the next attempt from becoming another guess. For this fabrication project, that kind of clarity is what turns a one-off success into a repeatable method instead of a lucky result. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
What Non-Ferrous Means
Non-ferrous metals are generally chosen when weight, corrosion resistance, conductivity, appearance, or specialized performance matters more than low-cost structural strength.
They are not automatically easier to fabricate. Some gum up cutting tools, some distort with heat, and some require special welding or finishing controls.
In a real fabrication workflow, non-ferrous often determines whether a project feels controlled or improvised. It affects setup choices before anyone reaches the final finish. For this fabrication project, this keeps the work practical and prevents the design intent from getting lost on the bench. It also gives the builder a specific thing to watch while non-ferrous moves from plan to shop work.
The safest approach is to confirm the feature while it can still be changed. Once parts are welded, coated, bonded, or delivered, small corrections become expensive. The review does not need to be formal; it needs to happen while the part can still be changed. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
Early confirmation can be as simple as a layout review, a gauge check, a scrap test, or a short conversation between the person designing and the person building. That makes non-ferrous easier to connect with material behavior, operator safety, and final quality in a way the whole team can follow. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
That feedback loop protects schedule and material. It also keeps the subject tied to decisions a maker can actually use in the shop. A clear record also helps future repairs, repeat orders, and design revisions move faster. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
Aluminum
Aluminum is light, corrosion-resistant, machinable, and available in many shapes and alloys. It is common in transportation, products, signage, frames, fixtures, and aerospace work.
Alloy choice matters. Some grades are easy to weld, some machine beautifully, and some gain strength from heat treatment that can be affected by fabrication.
Aluminum is worth slowing down for because it sits at the boundary between design intent and shop reality. That is especially useful when the same project involves several machines, materials, or finishing steps. It also gives the builder a specific thing to watch while aluminum moves from plan to shop work.
If the operation is rushed, the first warning may appear as rework: extra sanding, a stuck part, a poor joint, a warped edge, or a dimension that no longer matches the assembly. If aluminum creates trouble, the team can still adjust the sequence before the problem is buried under later cuts, coatings, or assemblies. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
A better workflow builds in a midpoint review. The part is checked while there is still time to adjust toolpath, pressure, heat, fixture location, or finish preparation. The lesson is more valuable when the change is measured, named, and connected to the result. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
That review does not make the job complicated. It keeps the work honest by connecting each visible detail to the process that created it. For this fabrication project, that makes the workflow sturdier without adding unnecessary complexity or slowing every future job. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
Copper, Brass, and Bronze
Copper is valued for electrical and thermal conductivity. Brass machines well and has a warm appearance. Bronze offers wear resistance and is common in bushings and bearings.
These metals often cost more than steel, but they solve problems steel cannot. Conductivity, corrosion behavior, low friction, and appearance can justify the choice.
For a maker or small shop, copper, brass, and bronze is often where experience turns into judgment. The drawing may name the feature, but the material decides how forgiving it will be. For this fabrication project, that judgment helps separate what must be controlled from what can vary safely. It also gives the builder a specific thing to watch while copper, brass, and bronze moves from plan to shop work.
Watching the first piece closely helps reveal whether the chosen process is stable. A clean result on one sample is useful only if the method can be repeated. The first piece is the best place to learn because it exposes problems before they multiply. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
Repeatability comes from boring habits that work: consistent setup, labeled parts, measured changes, clean surfaces, and tools that are maintained before they force a mistake. When copper, brass, and bronze is recorded clearly, the next setup begins with a shop record instead of a fresh guess about what worked last time. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
Those habits make the fabrication process easier to improve because every revision has a known starting point instead of a pile of disconnected fixes. That is how small fabrication habits become durable process knowledge. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
Choosing a Metal
The right metal depends on load, environment, weight, fabrication method, finish, availability, and budget. A strong material on paper may be wrong if it is hard to weld, machine, or protect.
Good material selection starts with failure mode. Rust, fatigue, bending, wear, heat, impact, and electrical needs all point toward different metals.
Choosing a metal is best judged by the finished use of the part. A decorative panel, structural bracket, mold, enclosure, or prototype may need a different level of control. That keeps the decision useful for the person making the part, not only for the person reviewing the drawing. It also gives the builder a specific thing to watch while choosing a metal moves from plan to shop work.
The shop can avoid overbuilding by asking which surfaces carry load, which edges are handled, which features locate the assembly, and which details mostly affect appearance. Early control over choosing a metal also reduces the temptation to hide a problem with extra finishing work after the core process has already drifted. That kind of early review is usually faster than repairing a finished part after the mistake is buried.
That question keeps cost and quality in balance. It helps the builder decide where to accept ordinary variation and where to tighten the process. The goal is a part that meets its purpose with the least amount of rework and confusion. For this fabrication project, the same habit supports cleaner communication between design, fabrication, inspection, and finishing.
Once that choice is made, the work becomes easier to explain, inspect, and repeat because the reason behind the detail is visible. For this fabrication project, that balance is often what separates a clean build from a frustrating one when the schedule gets tight. The payoff is a part that reaches the next step with fewer surprises and a clearer record of what changed.
Bottom Line on Types of Metals
Ferrous and non-ferrous metals each bring useful tradeoffs. The best metal choice comes from matching strength, weight, corrosion resistance, machinability, weldability, finish, and cost to the job.