Emerging CNC Technologies Are Changing Precision Fabrication
Emerging CNC technologies are reshaping fabrication by making machines more connected, more adaptive, and easier to monitor in real time. The core idea remains familiar: a tool follows a programmed path to remove or shape material. What is changing is how shops program jobs, verify setups, monitor cutting conditions, automate loading, and use data to make better decisions before scrap or downtime grows expensive.
A: Clear design intent, suitable material, controlled setup, safe workflow, and repeatable inspection.
A: It shows how the material and tool settings behave before the final part is at risk.
A: No. Tighter tolerance costs more and only helps when the function requires it.
A: Tool wear, speed, feed, abrasive choice, heat, vibration, or weak support can all contribute.
A: Heat, internal stress, uneven removal, poor clamping, or forming pressure can move material.
A: Use templates, mark clearly, cut oversize when appropriate, and inspect before each irreversible step.
A: Prototypes test ideas, while production work controls repeatability.
A: Surface prep, cleaning, masking, curing, and inspection often require more time than the main cut.
A: Ventilation and dust control are often overlooked until a process creates fumes or fine particles.
A: Confirm fit, function, finish, documentation, and any maintenance needs.
Smarter Programming and Simulation
Modern CAM software does more than convert geometry into toolpaths. It can simulate collisions, estimate cycle time, manage tool libraries, account for stock conditions, and preview where chatter or excess tool load may appear. That helps programmers catch problems before the machine is occupied.
Simulation is especially valuable when parts have deep pockets, tight clearances, five-axis motion, or expensive material. A verified program is not a guarantee, but it reduces surprises and gives the operator a clearer setup plan.
In shop terms, smarter programming and simulation affects how the fabrication work moves from a drawing into a part that can be held, cut, checked, and finished. For this fabrication project, that keeps the choice grounded in the actual build rather than a generic preference.
The detail deserves a small reality check before the next operation. A sample, dry fit, or first-piece inspection can show whether the plan is behaving as expected. A quick measurement or shop note at this point can prevent a much larger correction later and keep the next operation from hiding the problem.
That check gives the team a concrete signal instead of a vague impression. If fit, edge quality, release, alignment, or finish starts to drift, the process can be corrected early. It also makes responsibility clearer when design, setup, cutting, and finishing overlap.
The practical next step is to document the setting, mark the feature clearly, and keep the result tied to the drawing so the same choice can be repeated later. The result is a smarter programming and simulation decision that can be inspected, explained, and improved on the next run without rebuilding the whole plan.
Adaptive Machining and Tool Load Control
Adaptive machining strategies use smoother paths to keep tool engagement more consistent. Instead of burying the cutter in heavy corners, the toolpath manages chip load and avoids sudden spikes that can break tools or mark the part.
This matters for hard metals, deep roughing, and high-value components. When the cutting load stays steadier, shops can often improve tool life, surface quality, and cycle consistency while reducing the anxiety of aggressive cuts.
For this fabrication project, adaptive machining and tool load control is not an isolated detail. It influences material selection, setup time, tool access, and the amount of correction needed after the main operation. That keeps the work tied to fit, finish, safety, and cost instead of treating the detail as decoration.
A builder can treat this part of the work as a decision point: continue with the current setup, adjust the geometry, change the tool, or run a smaller trial first. When adaptive machining and tool load control is checked early, the builder has more options and less pressure to force a fix at the end after the part is already committed.
That decision is easier when the part is checked against the real stock and the real mating surfaces rather than only against an ideal model. It also gives the next person in the workflow a clearer reason for the chosen setup.
Good notes matter here because they turn one successful setup into a repeatable method for the next part, batch, repair, or revision. For this fabrication project, that record can be reused when the material, tooling, or quantity changes and the shop needs the same result again.
Probing, Measurement, and In-Process Checks
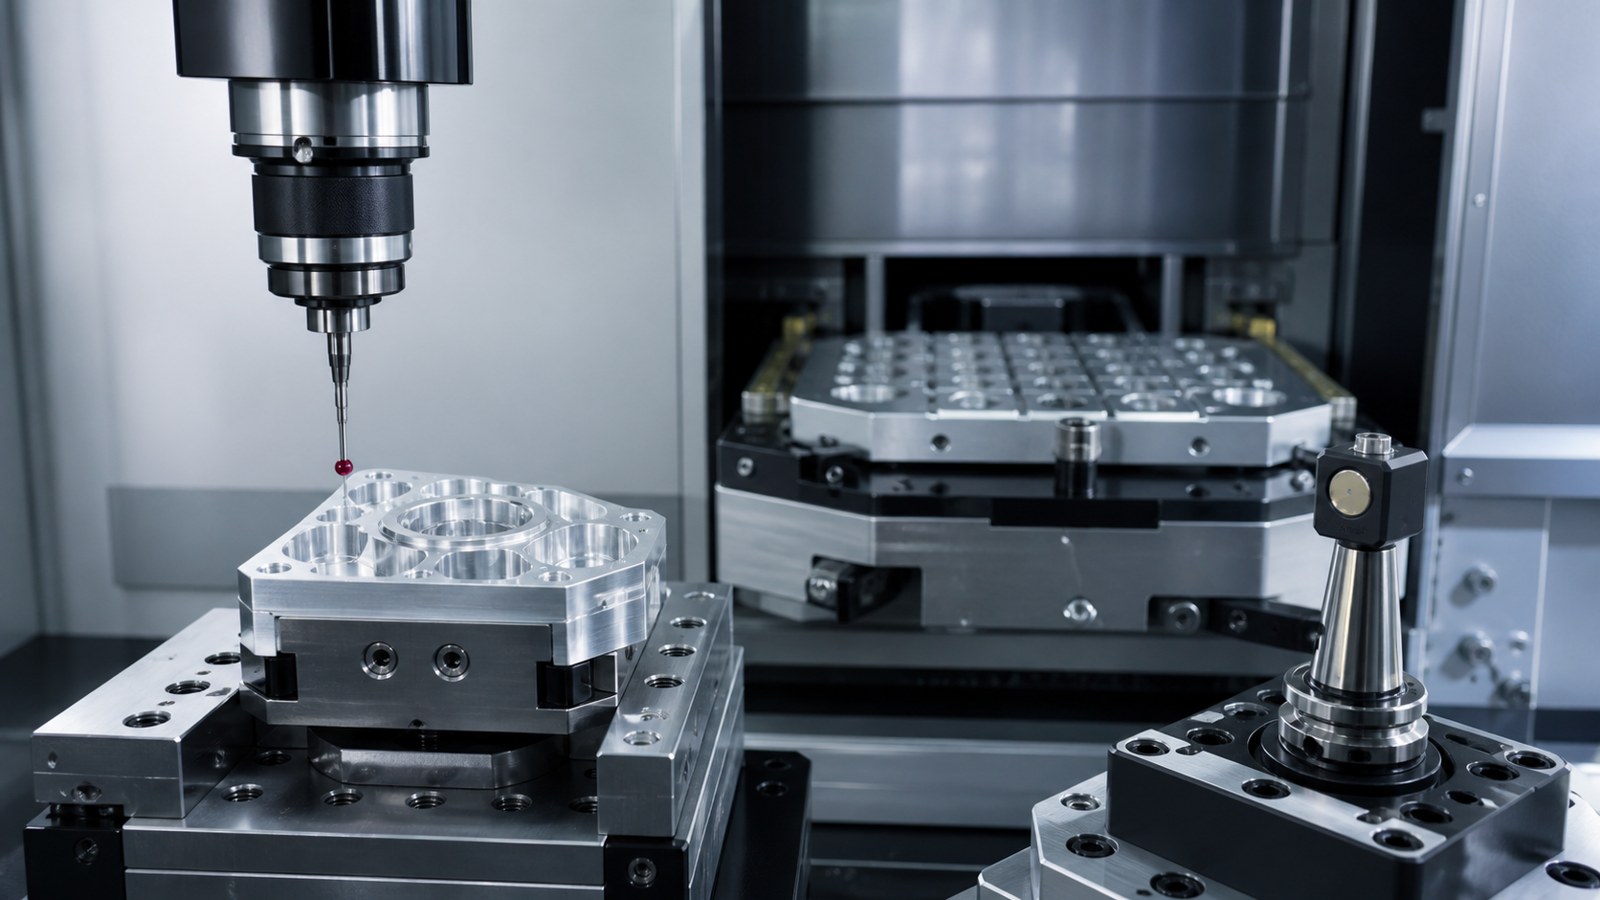
Machine probing has moved from luxury to practical production tool in many shops. A probe can locate stock, confirm a fixture, check a feature, update work offsets, or measure a critical surface before the part leaves the machine.
In-process measurement does not replace final inspection, but it shortens the feedback loop. If a part is drifting, the shop can respond before a full batch is wrong. That is especially important when tolerance, material cost, or delivery pressure is high.
The value of probing, measurement, and in-process checks becomes clear when the project reaches the bench. Small differences in thickness, radius, heat, clamp pressure, or surface prep can change the result. For this fabrication project, the payoff is fewer surprises when the part reaches assembly or finishing.
Instead of waiting for final assembly to reveal the issue, the shop can look for early signs: uneven fit, rough edges, distortion, poor release, or extra finishing work. A short pause here can protect the schedule because the correction is still small and visible.
Those signs help separate a design issue from a setup issue. The fix may be a cleaner drawing note, a different sequence, a new fixture, or a more suitable material. That makes probing, measurement, and in-process checks a practical control point instead of a vague shop preference, especially when multiple people touch the same job.
Handled this way, the topic becomes a working checklist rather than filler. It points to the specific shop condition that needs attention before the job advances. The next build starts from a known condition rather than from memory or guesswork.
Connected Machines and Shop Data
Connected CNC machines can report cycle time, spindle load, alarms, downtime, tool changes, and job status. That information helps supervisors see whether a bottleneck is programming, setup, tooling, maintenance, material flow, or operator availability.
Data only helps when it is used carefully. A dashboard full of numbers can still miss the real problem if the shop does not connect data to the part, fixture, material, and human decisions around the machine.
Connected machines and shop data also shapes communication. Designers, programmers, fabricators, and finishers need to know which surfaces matter and which dimensions have room to breathe. That context helps the team avoid spending time on details that do not change performance.
When that priority is clear, the shop can spend effort where it improves the finished part instead of chasing precision or polish in the wrong place. Checked early, connected machines and shop data can guide a better fixture, clearer drawing note, or cleaner finishing plan before the expensive steps begin.
The best review point is simple: compare the part to its function, not just to its appearance. Fit, strength, safety, and service conditions decide whether the work is ready. The process also becomes easier to teach because the reason behind the step is visible.
If the review exposes a problem, changing one variable at a time keeps the lesson useful. That habit prevents the next attempt from becoming another guess. For this fabrication project, that kind of clarity is what turns a one-off success into a repeatable method instead of a lucky result.
Automation and Robotic Loading
Automation is expanding through pallet systems, robotic loading, bar feeders, tool setters, and unattended machining cells. These systems can improve spindle utilization, but they require stable processes, good fixturing, and predictable chip control.
The biggest automation mistake is trying to automate a shaky process. If the program, fixture, material, or inspection plan is unreliable, automation may simply produce bad parts faster. Shops get better results when they stabilize the work first.
In a real fabrication workflow, automation and robotic loading often determines whether a project feels controlled or improvised. It affects setup choices before anyone reaches the final finish. For this fabrication project, this keeps the work practical and prevents the design intent from getting lost on the bench.
The safest approach is to confirm the feature while it can still be changed. Once parts are welded, coated, bonded, or delivered, small corrections become expensive. The review does not need to be formal; it needs to happen while the part can still be changed.
Early confirmation can be as simple as a layout review, a gauge check, a scrap test, or a short conversation between the person designing and the person building. That makes automation and robotic loading easier to connect with material behavior, operator safety, and final quality in a way the whole team can follow.
That feedback loop protects schedule and material. It also keeps the subject tied to decisions a maker can actually use in the shop. A clear record also helps future repairs, repeat orders, and design revisions move faster.
AI Assistance and Practical Limits
AI-assisted manufacturing tools can help with quoting, toolpath suggestions, anomaly detection, maintenance patterns, and documentation. The useful role is assistance, not blind control. CNC work still needs experienced people to understand material, sound, finish, and setup reality.
The best use of AI is to highlight patterns humans can review. A system might flag a rising spindle load or recurring alarm, while the machinist decides whether the cause is tool wear, coolant, stock variation, chip packing, or a fixture issue.
Ai assistance and practical limits is worth slowing down for because it sits at the boundary between design intent and shop reality. That is especially useful when the same project involves several machines, materials, or finishing steps.
If the operation is rushed, the first warning may appear as rework: extra sanding, a stuck part, a poor joint, a warped edge, or a dimension that no longer matches the assembly. If ai assistance and practical limits creates trouble, the team can still adjust the sequence before the problem is buried under later cuts, coatings, or assemblies.
A better workflow builds in a midpoint review. The part is checked while there is still time to adjust toolpath, pressure, heat, fixture location, or finish preparation. The lesson is more valuable when the change is measured, named, and connected to the result.
That review does not make the job complicated. It keeps the work honest by connecting each visible detail to the process that created it. For this fabrication project, that makes the workflow sturdier without adding unnecessary complexity or slowing every future job.
Hybrid Manufacturing and Multi-Process Cells
Some advanced systems combine additive and subtractive steps, or bring milling, turning, probing, laser marking, and inspection closer together. The goal is fewer handoffs and better control of part location between operations.
Hybrid thinking is useful even in smaller shops. Reducing setups, keeping references consistent, and designing fixtures around the full workflow can improve accuracy without requiring the newest machine on the market.
For a maker or small shop, hybrid manufacturing and multi-process cells is often where experience turns into judgment. The drawing may name the feature, but the material decides how forgiving it will be. For this fabrication project, that judgment helps separate what must be controlled from what can vary safely.
Watching the first piece closely helps reveal whether the chosen process is stable. A clean result on one sample is useful only if the method can be repeated. The first piece is the best place to learn because it exposes problems before they multiply.
Repeatability comes from boring habits that work: consistent setup, labeled parts, measured changes, clean surfaces, and tools that are maintained before they force a mistake. When hybrid manufacturing and multi-process cells is recorded clearly, the next setup begins with a shop record instead of a fresh guess about what worked last time.
Those habits make the fabrication process easier to improve because every revision has a known starting point instead of a pile of disconnected fixes. That is how small fabrication habits become durable process knowledge.
How Shops Should Adopt New CNC Tools
New CNC technology pays off when it solves a specific shop problem. A shop struggling with setup time may benefit from probing. A shop losing tools in roughing may benefit from adaptive strategies. A shop with idle spindles may need scheduling and fixturing before robots.
The smartest adoption path begins with one measurable target. Reduce scrap, shorten setup, improve inspection speed, extend tool life, or increase unattended hours. When the goal is clear, the technology is easier to evaluate honestly.
How shops should adopt new cnc tools is best judged by the finished use of the part. A decorative panel, structural bracket, mold, enclosure, or prototype may need a different level of control. That keeps the decision useful for the person making the part, not only for the person reviewing the drawing.
The shop can avoid overbuilding by asking which surfaces carry load, which edges are handled, which features locate the assembly, and which details mostly affect appearance. Early control over this detail also reduces the temptation to hide a problem with extra finishing work after the core process has already drifted.
That question keeps cost and quality in balance. It helps the builder decide where to accept ordinary variation and where to tighten the process. The goal is a part that meets its purpose with the least amount of rework and confusion.
Once that choice is made, the work becomes easier to explain, inspect, and repeat because the reason behind the detail is visible. For this fabrication project, that balance is often what separates a clean build from a frustrating one when the schedule gets tight.
Bottom Line on Emerging CNC Technologies
The future of CNC precision fabrication is not one magic machine. It is a stack of better programming, probing, monitoring, automation, data use, and operator judgment. Shops that connect new tools to real bottlenecks will gain more than shops that chase technology for its own sake.